 Galvatech Sdn Bhd


Three galvanizing methods, one specialist team
Hot-dip, hot-dip spun, and mechanical galvanizing, matched to your iron, steel, brackets, or fasteners and finished to BS EN ISO 1461:2009(E) or ASTM A123.
Hot-dip galvanizing
- Our kettle is sized at 4000mm (L) x 1000mm (W) x 1800mm (H)
- We provide hot-dip galvanizing service for both iron/steel products such as angle bar, c-channel, I-beam, flat bar, frames, railing, brackets and etc.
- We provide double dipping service for products up to 6 meter length
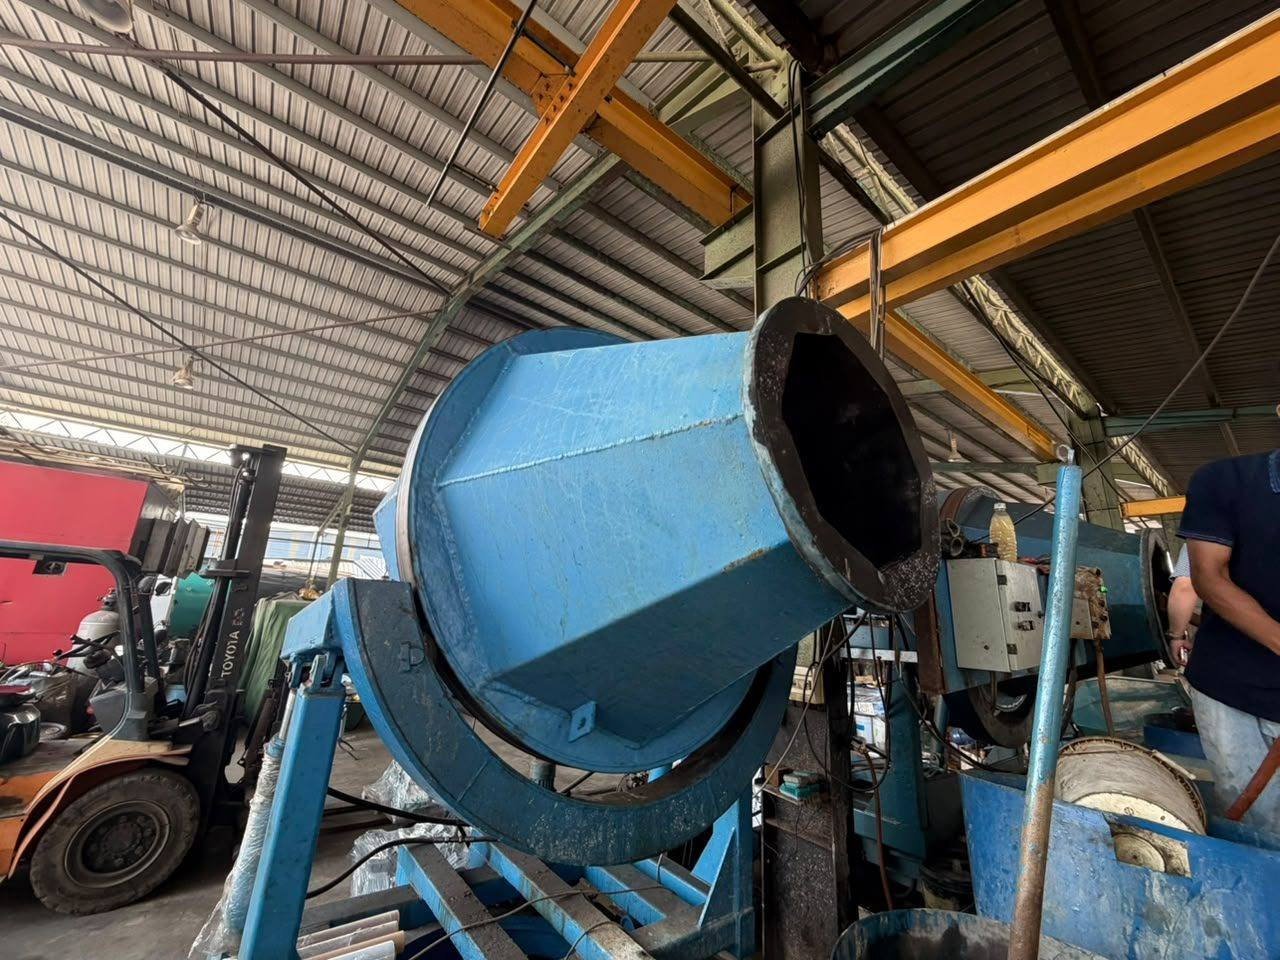
Hot-Dip Spun Galvanizing
- One of our specialties, mastered over more than 20 years of experience
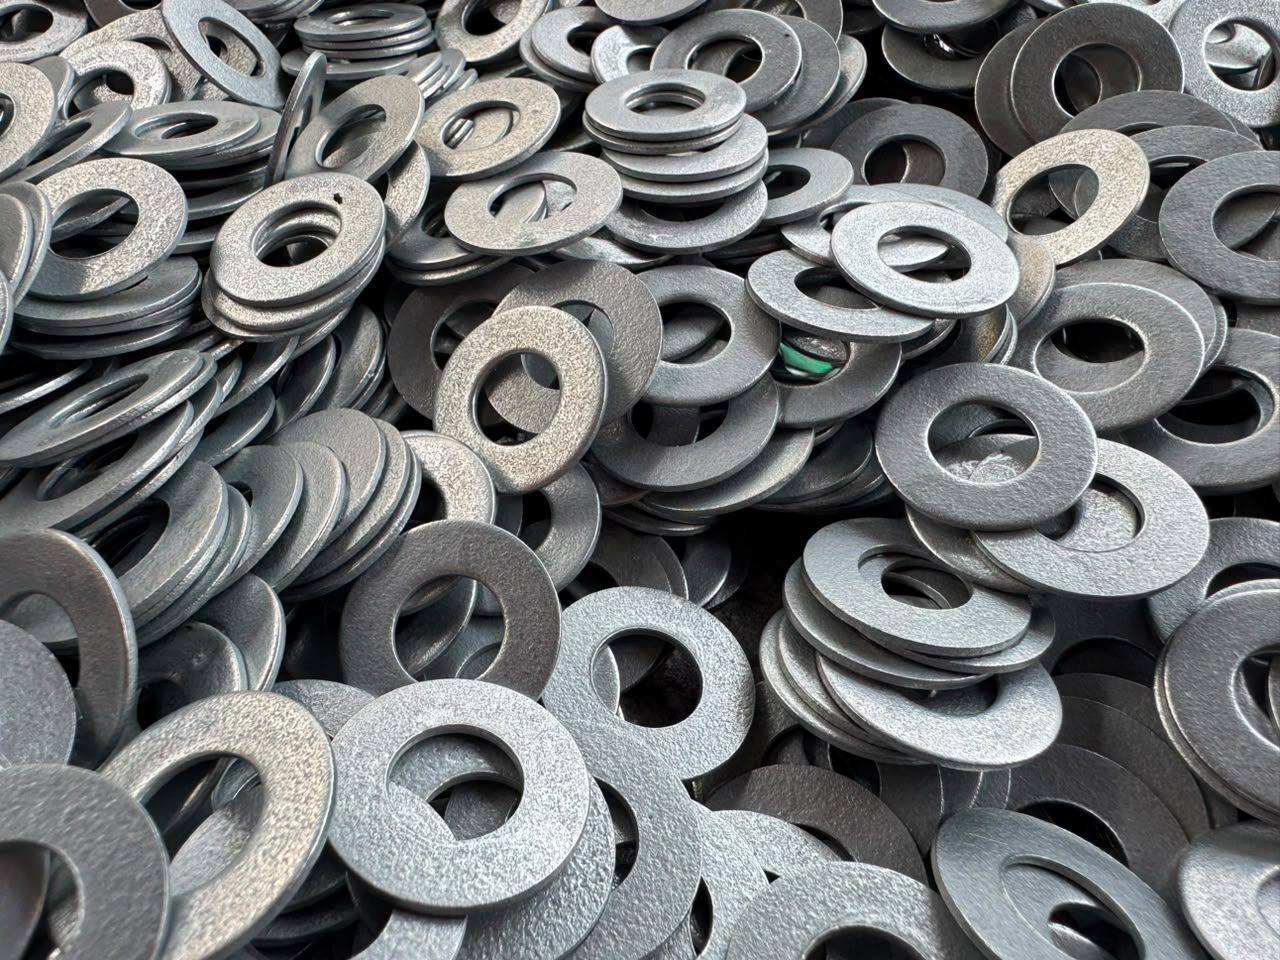
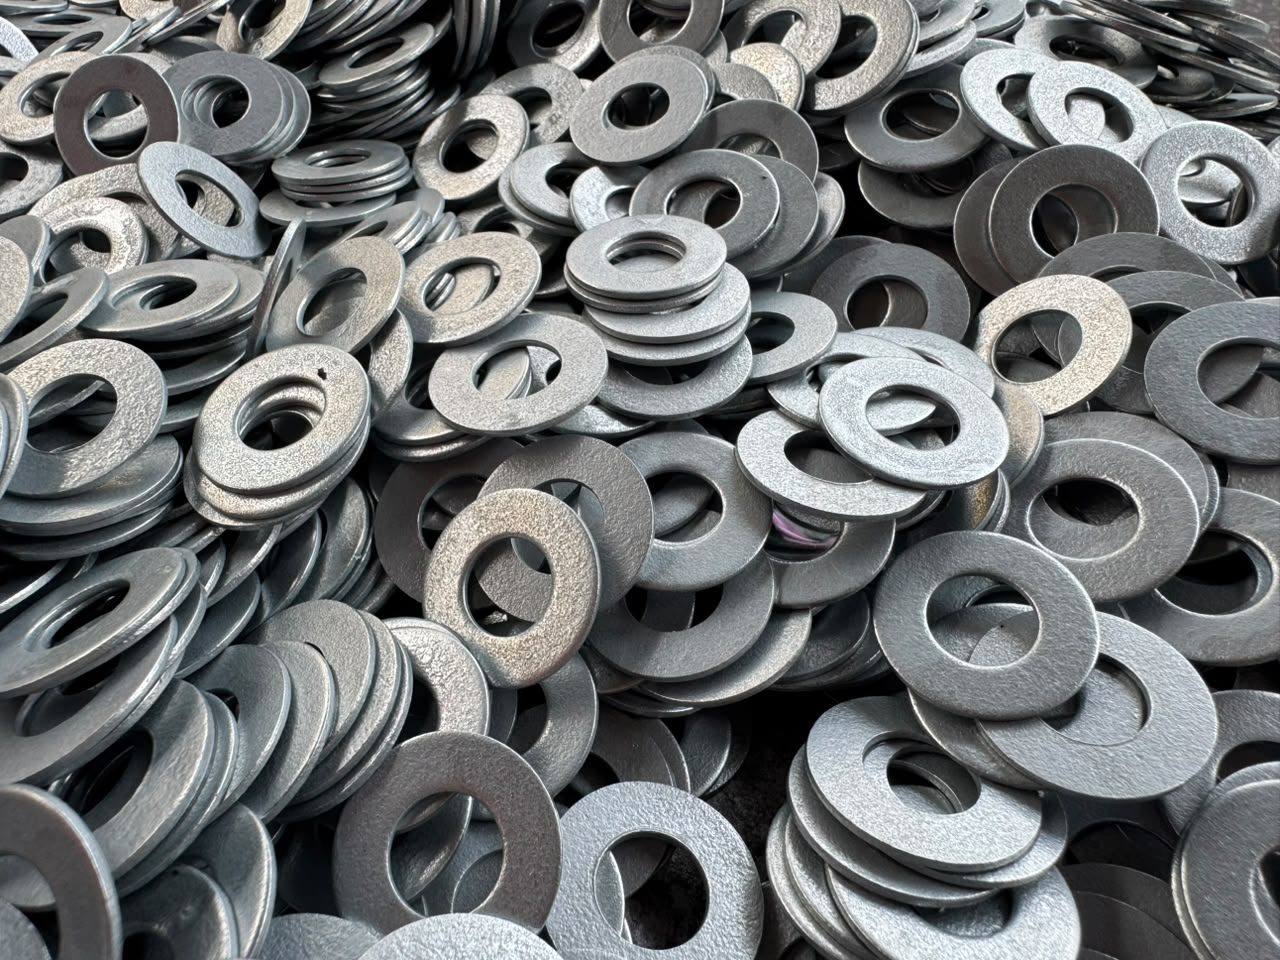
- For fasteners such as bolts, nuts, washers, and anchor bolts
- Special spun items up to M100 size, including fine-thread anchor bolts and cast iron brackets
Mechanical Galvanizing
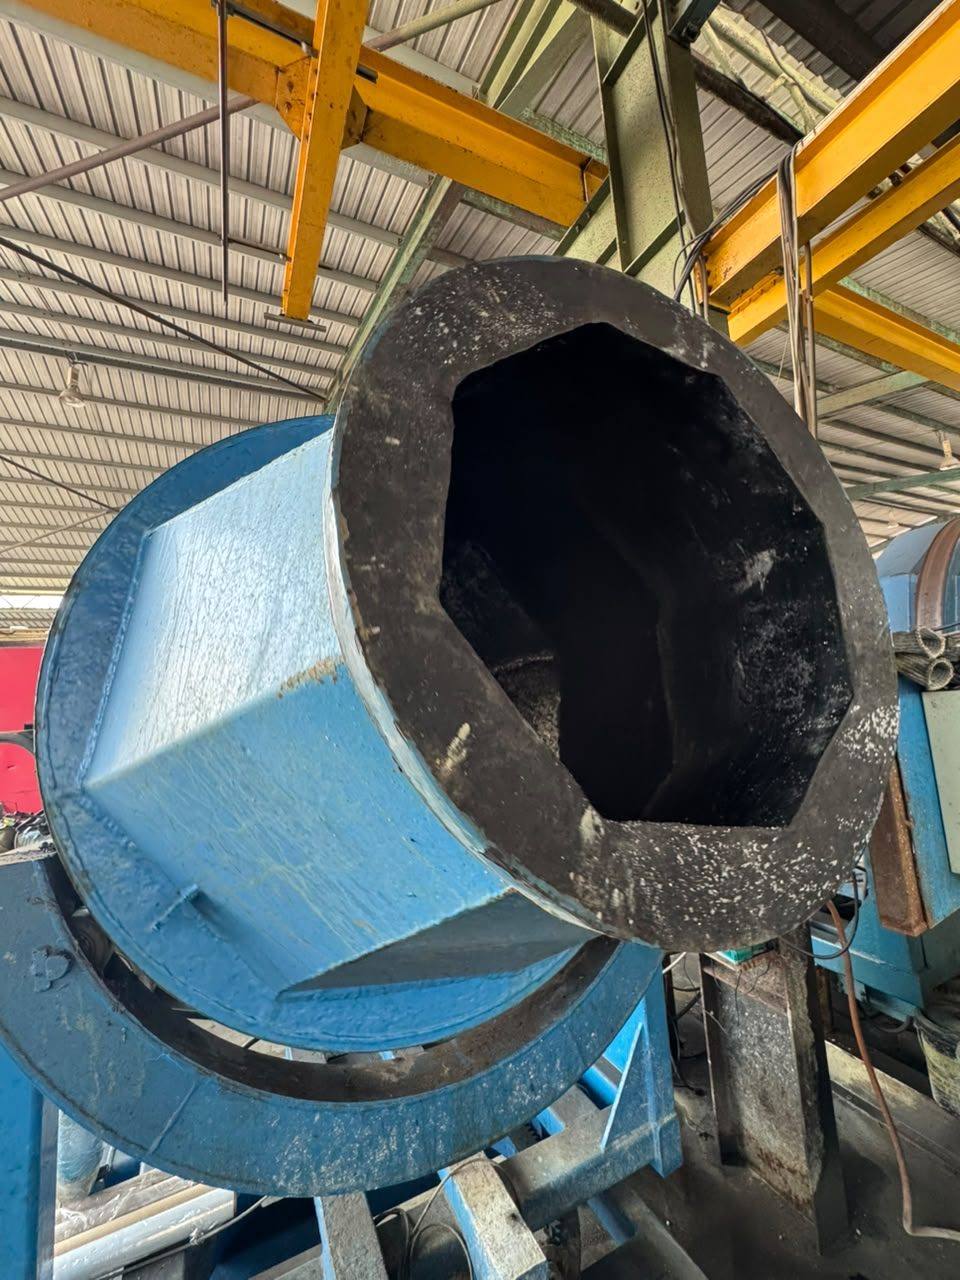
- No hydrogen embrittlement
- No detempering
- Excellent thread fit
- No chasing of nuts after plating
- No galling
- No stickers
- Excellent adhension
What happens to your steel
The same nine-step process, whether it's one bracket or a full site order.
-
Degreasing
Steel is degreased to strip oil, dirt, and grease from the surface.
-
Rinsing
Rinsed in water to clear degreasing residue before pickling.
-
Pickling
Dipped in acid to strip rust and mill scale down to bare metal.
-
Rinsing
Rinsed again to clear the pickling acid before fluxing.
-
Fluxing
A flux layer prepares the surface so zinc bonds evenly across every edge.
-
Drying
Product is dried before it enters the zinc bath.
-
Galvanizing
Full immersion in the molten zinc bath forms a metallurgically bonded coating.
-
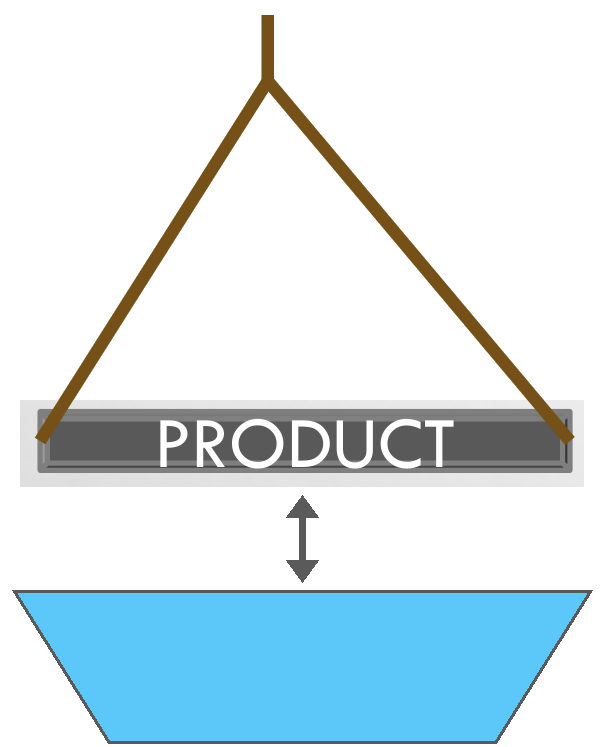
Quenching
Coated steel is quenched to cool and set the zinc layer.
-
Quality Check
Coating thickness is checked against BS EN ISO 1461:2009(E) or ASTM A123 before the batch ships.